October 2026 · About 4 minutes
Every assumption a PM makes before fabrication is a field problem that has not happened yet.
None of these are careless. Each one is a reasonable guess made by a busy PM with eleven other things open, and each one is right often enough to feel safe. Here are the five that cost the most when they are wrong, what you would actually watch happen, and what to check instead.
1. “The rough opening is probably right.” (It is not.)
The design dimension on the approved drawing says 8 feet 0 inches. The block mason was allowed a tolerance, the slab poured a little high at one corner, and the opening is 7 feet 11-1/4 at the sill and 8 feet 0-1/2 at the head. The frame built to 8 feet 0 does not go in. The crew either cuts it down on a jobsite saw, sends it back, or waits for a remake, and each of those costs more than the field measurement would have.
Check instead: a field dimension at three heights, plumb on both jambs, and level on the sill, or a guaranteed opening size from the GC in writing, before the release goes out. A drawing with “VIF” still on it is not released. When the opening does not match, the rough opening article walks through modify, send back, or remake.
2. “Hardware power supply routing is someone else’s concern.”
The door has a card reader and an electric strike on the schedule. The PM assumes the electrician will get power to it, the electrician assumes the glazier will leave a path in the frame, and the shop assumes nobody said anything because nothing is electrified. The frame arrives finished, with no path from the header to the strike, and someone drills through dark bronze anodize on the jobsite to run a wire that should have gone through bare extrusion in the shop.
Check instead: confirm every electrified device with the hardware supplier before release, and put the wire path on the drawings so the shop preps it before finish. The electrified door hardware article covers the path from the supply to the device, and the entrance release article covers the other five door details that change the prep.
3. “The field can make it work.”
The frame is 3/8 narrow, the crew has a chop saw, and the foreman says he can take it out of the sill. He can. The cut is not quite square, the weep slots move, the finished sill face picks up a scratch in the handling, and the door jamb that was prepped for pivots at a specific height is now 3/8 off the threshold it was prepped for. The field fix created two more field fixes and a finish claim.
Check instead: before any field modification, ask whether the cut moves a hardware prep, a pivot, or a weep; whether the cut edge will show; and whether the crew would be freehanding something the shop does on a machine. If any answer is yes, the fix belongs in the shop. Field modification is right when the cut is simple and the edge is hidden, and wrong the rest of the time.
4. “The finish is close enough.”
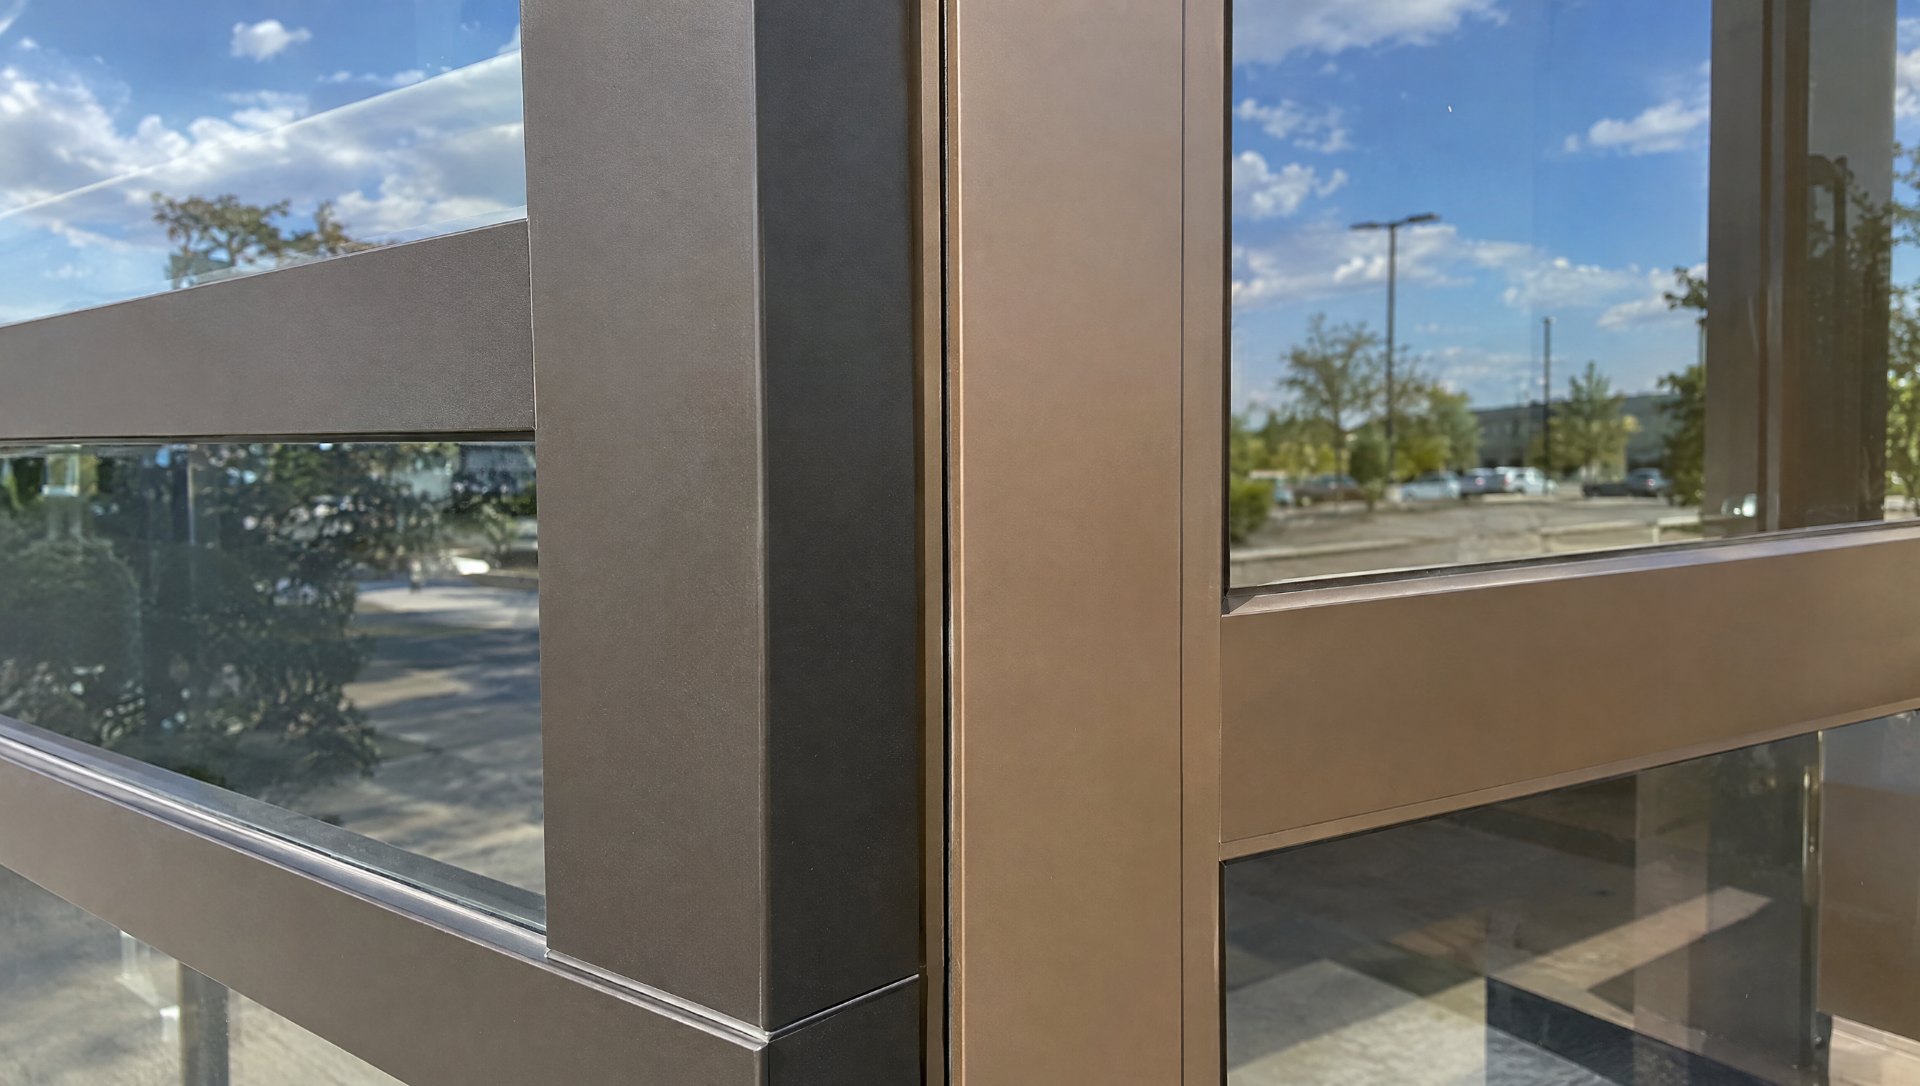
The spec says dark bronze. The frames were anodized at one finisher and the doors were painted a bronze PVDF because the door supplier’s finisher was faster. Side by side at the entrance in afternoon light, they are two different colors, and the architect sees it on the walk-through. The doors go back through the whole finishing cycle, and the opening sits with temporary plywood for three weeks.
Check instead: the finish schedule names the type (Class I or Class II anodize, two-coat or three-coat paint, powder coat), the color by the manufacturer’s name and number, and the finisher, for every component, before anything is ordered or cut. If frames and doors are finished in two places, somebody signs off on a sample of each next to the other. Once the finish is on and gets hit in shipping or on site, the scratch repair article covers what can and cannot be fixed.
5. “The fabricator will figure it out.”
The release says “per hardware schedule,” “finish per spec,” and “doors per elevation.” The shop can read none of those. It does one of two things: stops and asks, which costs a week of back-and-forth while the package sits, or decides, which is a remake waiting to happen when the decision was not the one the PM would have made. Neither is the fabricator’s fault. The release handed him a guess.
Check instead: list what is missing, in writing, and send it with the release as open items, or hold the affected openings until it is closed. The fabrication release article lays out what a complete release contains, document by document, and the five-item checklist is the one-minute version.
The takeaway
Every assumption made before fabrication becomes a potential field problem, so verify the details that are hardest and most expensive to correct later: the opening, the power, the modification, the finish, and the missing information. Each one takes minutes to check before release and weeks to fix after.
WestMetal Fabrication reads every release for the assumption in it before cutting, and asks once, in one list, rather than guessing. See what WestMetal fabricates.
Learn the fundamentals on LearnGlazing
Two free LearnGlazing courses cover the ground this article skips. Introduction to Fabrication walks through shop operations and delivery considerations, and Introduction to Door Hardware explains knocked-down, shop-assembled, and pre-glazed packaging. WestMetal Group is a LearnGlazing partner through the GlazierIQ network. Browse the full course catalog.
Bob Baumann
Sales, WestMetal Group
I have been on the fabrication side of glazing for a long time, and before WestMetal I ran a shop floor where the release was the thing that decided whether the week went well or badly. I still read every package that comes in before it goes to the saw, and I still call the PM when something on it does not add up. WestMetal Group is part of the GlazierIQ network with MP Drafting and LearnGlazing. Questions about an article or a package? Send it to Bob.
</div >